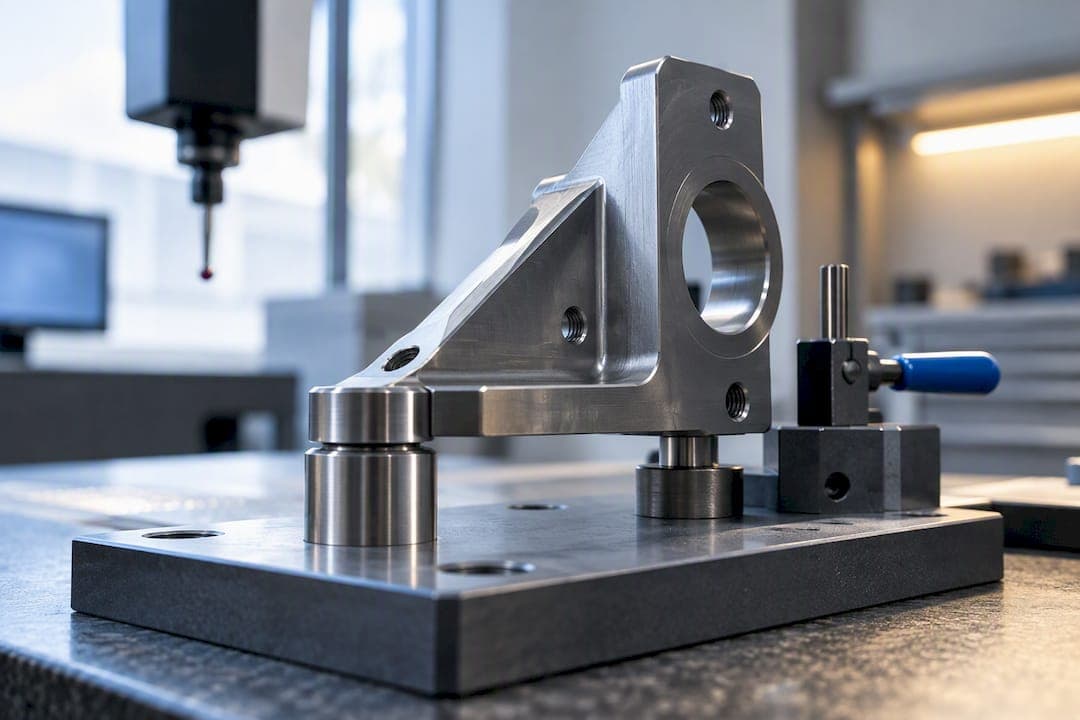
Pick datum features by function first: the features that actually locate or constrain the part in assembly become datum A, B, and C, in that order of contact priority. Once you have that sequence, confirm each candidate is large enough, physically accessible, and repeatable under a probe or fixture. If a surface fails on size or repeatability, replace full-surface contact with datum targets and document the datum establishment method in your inspection record, because that documentation is what protects you when a measurement gets challenged later.
TL;DR:
- Ensure functional datums are chosen based on their actual role in assembly, not just their surface appearance or ease of measurement.
- Verify primary datums are large and stable enough to resist movement, with size considerations prioritizing resistance to rocking or tipping.
- Confirm accessibility so probes or fixture pins can physically reach the datums without obstruction, reducing measurement variability.
- Follow the 3-2-1 rule by sequencing datums A, B, and C to remove all degrees of freedom reliably, considering functional importance and measurement complexity.
- Document the datum establishment method, fixture setup, and measurement procedures thoroughly to ensure repeatability and defend measurement results later.
Table of Contents
- What Datum Selection Inspection Actually Requires
- Datum Selection Rules: Prioritize Function, Size, Accessibility, Repeatability
- Primary, Secondary, Tertiary Sequencing And The 3-2-1 Rule In Practice
- Datum Targets: When To Use Them And How They Become Fixture Hardware
- Reproducing The DRF On CMMs And Shop Fixtures
- Common Traps And Quick Fixes From The Inspection Floor
- Documentation, Uncertainty, And Audit-Ready Reporting
- Why Inspection Needs A Seat At The Design Table
- How QA-Report Keeps Your Datum Decisions Consistent On Every Report
- Sources
- FAQ
What Datum Selection Inspection Actually Requires
Datum selection inspection is the practice of verifying that a part's datum reference frame, or DRF, is established the same way on the inspection fixture or CMM as it was intended on the drawing. It sounds like a formality until you've watched two inspectors get two different pass/fail results on the identical part because one clamped a casting on its rough boss and the other used a machined pad thirty millimeters away. Both followed the drawing. Only one followed the design intent.
ASME Y14.5 is the standard that governs how datums, datum features, and datum targets get defined and referenced, and it exists precisely because "pick a flat spot" is not an inspection method. The standard treats a datum as a theoretically exact plane, axis, or point, established from a real, imperfect physical feature. Your job during datum selection criteria review is closing the gap between that theoretical reference and the actual surface a probe or fixture pin touches.
Most datum disputes on the shop floor trace back to one of two root causes: the designer picked a datum that never gets reliably contacted in production, or the inspector's fixture doesn't reproduce the DRF the designer intended. Both are preventable, and both get cheaper to fix the earlier you catch them. That's why datum selection deserves attention during design review, not just during first article inspection.
Datum Selection Rules: Prioritize Function, Size, Accessibility, Repeatability
Good datum selection criteria come down to four questions, applied in order. Skip the order and you'll end up defending a DRF that looks correct on paper but falls apart on the fixture.
Function comes first. A functional datum is the feature that actually mates, locates, or constrains the part when it's installed or assembled. If a bracket bolts to a bulkhead through two clearance holes and sits against a flange face, that flange face and those holes are your functional datums, not whatever flat surface happens to face up on the machine table. Functional datum selection means the DRF mirrors the constraint the part experiences in service, so a part that passes inspection also behaves correctly in the assembly it was designed for.
Size and stability come second. A primary datum needs enough contact area or length to resist rocking, tipping, or shifting under normal handling and probing force. Industry guidance built around ASME's sufficient-size requirement points out that undersized primary datums produce unstable reference frames. That instability shows up as measurement variability that has nothing to do with the part's actual geometry and everything to do with how it happened to sit that particular time. A three-millimeter boss makes a poor primary datum no matter how central it looks on the drawing.
Accessibility determines whether you can actually build a fixture around the choice. An internal bore that's perfect functionally but buried behind three other features forces awkward probe angles, custom tooling, or partial contact that undermines repeatability. Before you commit to a datum, sketch out how a CMM probe or a fixture pin physically reaches it. If the answer involves a six-inch extension probe reaching past a wall, reconsider, or plan for a datum target instead of full-surface contact.
Repeatability closes the loop. A rough casting surface, an as-forged boss, or an uneven weldment face will give you a different contact point almost every time you set the part down. That's not a probing problem, it's a surface condition problem, and the fix isn't a better fixture. The fix is switching to datum targets, which specify exact contact points instead of asking the whole surface to behave.
Here's a quick checklist you can run against any candidate datum before it goes on the drawing or into your inspection procedure:
- Does this feature actually locate or constrain the part in its mating condition?
- Is the contact area or length large enough to prevent rocking or tipping?
- Can a probe or fixture pin physically reach this feature without obstruction?
- Will this feature contact the same points every time the part is loaded?
- Does the surface condition (cast, forged, machined) support reliable point contact, or does it need targets?
If you answer "no" to any of the last three, you're not necessarily choosing the wrong datum. You're choosing the wrong contact method for that datum.
Pro Tip: Run the checklist during design review, not during first article inspection. A datum that fails the accessibility test is far cheaper to fix on a drawing redline than after your fixture is already machined.
Primary, Secondary, Tertiary Sequencing And The 3-2-1 Rule In Practice
Every datum in a DRF removes degrees of freedom, and the classic 3-2-1 rule tells you exactly how many each level should take. Datum A, the primary datum, removes three degrees of freedom by contacting a plane at three points, which stops the part from rotating in two directions and translating along one axis. Datum B, the secondary, removes two more degrees of freedom through a line of contact, typically stopping rotation around the remaining axis and translation in a second direction. Datum C, the tertiary, removes the last degree of freedom with a single point of contact, locking translation in the final direction.

A machined bracket sitting flat on a mill table (A), pushed against a fence (B), and stopped by a single pin (C) is the textbook version of this sequence. In practice, most datum reference points work exactly this way: a broad flat face for A, an edge or slot for B, and a hole or small pad for C.
Composite or simultaneous datum requirements come into play when a single feature pattern, like a bolt circle, needs to establish more than one datum simultaneously rather than in strict sequence. This shows up often in flange-mounted components where the bolt pattern itself defines both rotational orientation and center location at once. Treat these callouts carefully during inspection programming, since a CMM routine that processes them sequentially instead of simultaneously will compute a different, and wrong, DRF.
Deciding whether to keep the drawing's A-B-C order or consider an alternate sequence like B-A-C requires weighing function against inspection complexity. Follow these steps when the sequence isn't obviously dictated by the assembly:
- Identify which feature constrains the most critical functional relationship, usually alignment or mating fit, and make that datum A regardless of its position on the drawing.
- Confirm the secondary datum controls rotation around the axis datum A didn't already fix, without duplicating constraint.
- Verify the tertiary datum removes only the single remaining degree of freedom, and nothing more.
- Check whether swapping the order (B-A-C, for instance) would simplify fixture design without changing which functional relationships get controlled.
- If a swap changes measured results on toleranced features, flag it. That's a sign the original sequence carries functional weight the swap would break.
- Document the final order and rationale in your inspection procedure so a different inspector reaches the same DRF a year later.
Datum order isn't cosmetic. Reversing A and B on a part with a long, narrow secondary feature can change how much angular error the DRF tolerates, which changes what passes and what fails on the exact same physical part.
Datum Targets: When To Use Them And How They Become Fixture Hardware
Datum targets exist for exactly the surfaces that fail the repeatability test: castings, forgings, large flanges, and any feature where full-surface contact would give you a different answer every time. Instead of asking the entire surface to serve as the datum, ASME Y14.5 lets you specify exact points, lines, or areas of contact, and the 3-2-1 rule still applies underneath: three point targets typically establish a primary datum plane, two establish a secondary line, and one establishes the tertiary point.
You'll need datum targets in a handful of recurring situations:
- A cast or forged surface with too much variation for reliable full-surface contact.
- A large flange or sheet-metal panel that would rock or flex under three-point support if the points weren't specified precisely.
- An assembly where only a small, localized area of a bigger surface actually contacts a mating part, so contacting the whole surface would misrepresent the functional condition.
- A part with a draft angle or taper where a fixed-position target needs to move along a defined path to maintain contact.
Specifying targets correctly matters as much as choosing to use them. Target locations get basic dimensions, not tolerances, because the target location itself is theoretically exact, just like any other datum reference. A common drafting error is applying a plus/minus tolerance to a target's position, which contradicts the entire concept and confuses whoever has to program the CMM or build the fixture later.
Translating targets into fixture hardware is where the design finally becomes physical. A point target usually becomes a spherical-tip pin. A line target becomes a knife edge or a narrow rail. An area target becomes a flat pad sized to match the specified contact zone, no larger. For tapered features, movable or spring-loaded targets maintain contact as the part's geometry shifts along the taper, which keeps the DRF stable even though the physical location isn't fixed.

Reproducing The DRF On CMMs And Shop Fixtures
The drawing's datum reference frame only matters if your fixture and your CMM program actually reproduce it. That mapping happens in three stages: the drawing defines the datum, the fixture or CMM setup implements it physically or programmatically, and the measurement software fits the collected points back to a substitute geometry that's supposed to represent that same datum. Break the chain at any stage and your inspection results describe a part that doesn't exist.
This is where sampling strategy and fitting algorithm choice stop being academic concerns. NIST research on measurement uncertainty documents that sampling pattern and algorithm selection, least-squares versus min-max being the most common comparison, materially change the computed geometry from the exact same physical part. Two CMM programs measuring identical points with different fitting math can report different flatness values, different datum plane orientations, and ultimately different pass/fail decisions.
That sensitivity is why NIST's follow-on work on digital datum establishment points toward constrained least-squares fitting as an emerging middle ground, balancing the numerical stability of standard least-squares against the mechanical realism of min-max approaches. If your CMM software offers a choice of fitting algorithm for datum features, that choice belongs in your documented procedure, not left to whatever the software defaults to.
Run through this checklist before trusting a CMM-generated DRF:
- Confirm probe point count and placement match a documented strategy, not an ad hoc scatter across the surface.
- Verify fixture stiffness under probing force; a fixture that flexes under contact pressure introduces error the software will never catch.
- Check environmental conditions, particularly temperature, for parts with tight tolerances or dissimilar materials.
- Confirm the CMM's fitting algorithm matches what the drawing's datum definition assumes.
- Validate calibration records are current for the probe and the machine.
Pro Tip: When a part fails inspection but assembles without issue on the shop floor, don't assume the assembler got lucky. Check your sampling density and fitting algorithm first. A measurement artifact from too few probe points or a mismatched fitting method produces false rejects that look exactly like real out-of-tolerance conditions.
One in-house habit worth adopting: whenever a new fixture or CMM program goes into service for a critical datum, validate it against a physical assembly mockup at least once. NIST's uncertainty research makes clear that sampling and algorithm effects are real and measurable, not theoretical edge cases, which means a part that measures out-of-tolerance on one program and in-tolerance on another isn't necessarily a manufacturing problem. Sometimes it's a measurement setup problem, and the only way to know which is to check against how the part actually behaves in its intended assembly.
Common Traps And Quick Fixes From The Inspection Floor
Most datum-related rejects trace back to a small set of repeat offenders. Recognizing the pattern is faster than diagnosing each incident from scratch.
Non-functional datum choice. A designer picks the surface that's easiest to dimension from, not the surface that actually locates the part in assembly. The fix is a design review pass specifically asking "what surface does this part actually rest against when installed?" and revising the DRF to match. This is the single most common root cause behind parts that pass inspection but fail to assemble.
Undersized primary datum. A small boss or pad gets designated datum A, and the part rocks slightly every time it's loaded onto the fixture. The fix usually isn't finding a bigger surface elsewhere on the part. It's adding a flatness callout to control the surface's own quality, or converting to datum targets that specify a wider, more stable point pattern.
Undocumented datum targets. A target gets used on the shop floor, maybe informally agreed between the designer and the fixture builder, but never makes it onto the drawing or into the inspection procedure. Six months later, a different inspector measures the same part differently, and nobody can explain why. The fix is procedural: every target gets a basic-dimensioned location on the drawing and a corresponding note in the inspection plan, full stop.
Mismatched datum order between drawing and CMM program. The drawing calls out A-B-C, but the CMM program, written months earlier for a similar part, still references the old sequence. The fix is a program review triggered any time a drawing revision touches the datum callout, not just when the toleranced dimensions change.
A quick before-and-after: a cast housing originally used its as-cast mounting flange as datum A, and inspectors reported inconsistent flatness readings from batch to batch. Switching to three area targets on the flange, specified with basic dimensions and matched to the actual bolt-circle contact zones, eliminated the variability because the inspection now measured the same three points every time instead of an uneven surface that changed shape slightly with each casting run.
Documentation, Uncertainty, And Audit-Ready Reporting
Datum selection inspection doesn't end when the CMM reports a number. It ends when that number is defensible months later to an auditor, a customer, or a different inspector running the same part. That defensibility depends on documentation most teams under-invest in.
Measurement uncertainty has contributors beyond equipment tolerance. Sampling strategy and fitting algorithm choice are measurable, controllable sources of variation, not background noise. NIST's uncertainty research treats these as first-order factors worth documenting, not footnotes.
A control plan or first article inspection package should capture:
- The datum establishment method, including which physical features or targets served as A, B, and C.
- Fixture sketches or photos showing pin, pad, and target locations.
- The CMM fitting algorithm used for each datum feature.
- Sampling strategy, including probe point count and pattern.
- Current calibration records for the probe and machine used.
Recording fixture settings, datum targets, and the CMM mapping used for each report is what keeps two inspectors, a year apart, arriving at the same conclusion about the same part. Without it, every disputed measurement becomes a debate instead of a lookup.
This is precisely the gap QA-Report's own guidance on datum reference frames addresses, and it's built into how the platform structures inspection reports. Automatic drawing ballooning can link each toleranced dimension to its measured result, so the datum callouts stay attached to the actual measurement rather than living separately in an inspector's notes. CMM data import can pull sampling and fitting details directly into reports instead of requiring manual re-entry. Tolerance validation can flag out-of-tolerance conditions automatically, and resulting FAI reports aim to capture the full chain from drawing datum to fixture to measured result in one document.
Capture datum targets, fixture settings, and inspection-state notes in every report, not just the ones that fail. The reports that pass without incident are exactly the ones you'll need later to prove your process was consistent all along.
Why Inspection Needs A Seat At The Design Table
The best datum decisions I've seen come from design reviews where an inspector or quality engineer was in the room before the drawing got released, not after. Designers optimize for function and manufacturability. Inspectors know which surfaces actually hold still on a fixture and which ones will haunt a CMM program for years. Both perspectives are necessary, and skipping the second one is how functionally sound designs end up with datums nobody can measure consistently.
If your team has the option, verify a proposed DRF against a physical assembly mockup before it's frozen. It catches mismatches between design intent and fixture reality faster than any amount of drawing review.
Three priorities matter most once a part is in production: document the datum establishment method every time, train operators on exactly where fixture contact points are supposed to land, and keep datum order consistent between the drawing and every downstream inspection program. Consistency, not cleverness, is what makes a DRF trustworthy across a production run that might last years and involve a dozen different inspectors.
— Michael Chen
How QA-Report Keeps Your Datum Decisions Consistent On Every Report
QA-Report is built for exactly the failure mode this article describes: a correct datum choice on paper that turns into inconsistent measurements because the fixture, the CMM program, and the inspection report never got tied together. Automatic drawing ballooning links every toleranced dimension, including datum callouts, straight to its measured result, so the DRF an inspector used is visible on the report itself instead of buried in someone's memory.
CMM data import brings sampling and fitting details into the same report automatically, cutting the manual re-entry that introduces transcription errors on high-mix production floors. Tolerance validation auto-flags out-of-tolerance deviations the moment measured results come in, and the platform generates FAI and AS9102-ready reports that satisfy ISO 9001, AS9100, and PPAP documentation requirements without hours of manual formatting. Mobile access means an inspector on the floor can log datum target contact points and fixture notes in real time, not reconstruct them from memory at a desk later.
The practical payoff is fewer false rejects traceable to inconsistent DRF setup and faster inspection cycles because ballooning and validation happen automatically instead of by hand. QA-Report offers a Free plan alongside Basic and PRO tiers on its pricing page, so a quality team can start documenting datum establishment methods on their next first article inspection without committing to a long evaluation cycle first.
Sources
The guidance in this article rests on a small set of sources worth keeping in your own inspection procedures and training materials, not just this page.
- ASME Y14.5-2018 (standard overview)
- NISTIR 5170 — Measurement uncertainty and sampling/fitting effects
- OpenExamPrep — Functional datum feature selection (study guide)
Save these alongside your control plans and FAI templates. Standards get revised and software evolves, but the underlying principle, function before convenience, stays constant.
FAQ
What Are The Three Types Of Datum?
The three datum levels are primary (datum A), secondary (datum B), and tertiary (datum C), each removing a specific number of degrees of freedom under the 3-2-1 rule. Primary removes three degrees of freedom through plane contact, secondary removes two through line contact, and tertiary removes the final one through point contact.
How Do I Select A Datum?
Select datums by function first, choosing the features that actually locate or constrain the part in its mating or assembled condition. Then confirm the candidate feature has sufficient size for stability, is physically accessible to a probe or fixture pin, and produces repeatable contact, using datum targets when the surface condition makes full contact unreliable.
How Do You Select Datums In GD&T?
GD&T datum selection follows ASME Y14.5's framework: identify the functional datum reference points that establish the part's orientation and location in assembly, sequence them A-B-C based on which removes which degrees of freedom, and specify datum targets wherever a rough or uneven surface can't provide reliable full-surface contact. A tool like QA-Report can help keep that sequence consistent between the drawing and every CMM program that measures against it.
What Is The Purpose Of A Datum?
A datum establishes a theoretically exact reference plane, axis, or point that ties measurements, tolerances, and manufacturing setups back to the same consistent frame of reference. Without a shared datum reference frame, two people measuring the same part could reach different, equally defensible conclusions about whether it's in tolerance.
Why Do Some Parts Need Datum Targets Instead Of Full-Surface Datums?
Datum targets replace full-surface contact when a surface's condition, such as an as-cast or forged finish, makes repeatable contact unreliable across multiple inspections. Specifying exact point, line, or area targets with basic dimensions guarantees the same contact locations every time, regardless of surface roughness elsewhere on the part.