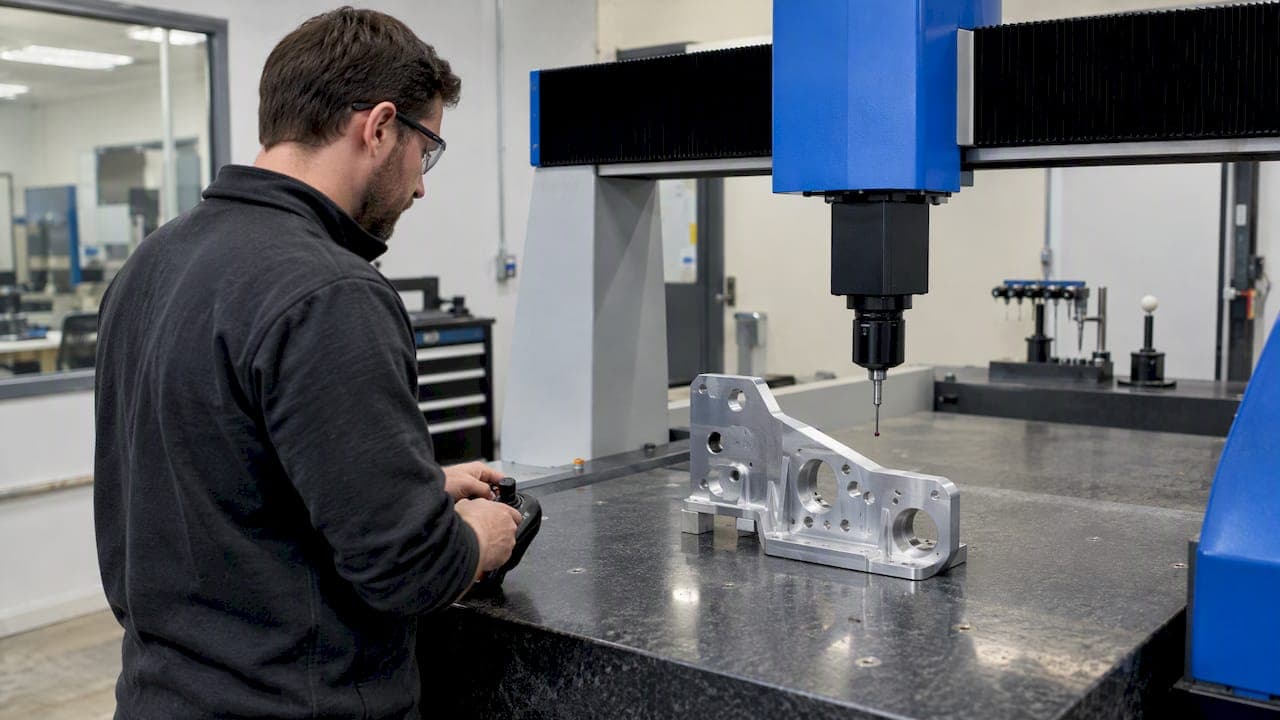
Bonus tolerance is the extra positional allowance a feature of size earns when it departs from its MMC or LMC. The arithmetic is simple: bonus equals actual size minus MMC for a hole, and total position tolerance equals the specified tolerance plus that bonus. Under ASME Y14.5, only features carrying an M or L modifier qualify.
TL;DR:
- Apply bonus only to a feature of size when its frame shows a circled M or L; without either modifier, position tolerance remains fixed.
- MMC bonus grows away from the most material size, while LMC bonus grows away from the least material size; each reaches full feature size tolerance.
- The virtual condition stays fixed as bonus grows; a functional go gage checks that boundary, while CMM software must apply the drawing’s modifier correctly.
- Inspectors must check size and position independently, compare diametral deviation with diametral tolerance, and record actual size, bonus, total allowance, standard, and measurement method.
- Confirm the governing standard and revision, and distinguish a modifier on the controlled feature from datum modifiers, which permit separate datum shift.
Table of Contents
- When does bonus tolerance apply, and why do designers use it?
- How do MMC and LMC generate bonus tolerance?
- How do you calculate bonus tolerance and total position tolerance?
- What are virtual condition and functional gages, and how do they relate to bonus?
- How do you read the feature control frame for bonus tolerance?
- What does bonus tolerance change in inspection and CMM workflows?
- Which quick examples build the habit?
- An editorial view on choosing MMC or LMC
- How QA-Report supports bonus tolerance inspection
- FAQ
- Sources
When does bonus tolerance apply, and why do designers use it?
Bonus tolerance exists only when two conditions are met. The controlled feature must be a feature of size, such as a hole, a shaft, a slot or a tab. And the feature control frame must carry a material condition modifier, either the circled M for maximum material condition or the circled L for least material condition. Remove either condition and the bonus disappears.
When no modifier appears in the frame, ASME Y14.5 treats the control as Regardless of Feature Size (RFS). Under RFS the positional tolerance stays fixed at its stated value no matter how the feature size varies within its limits. Designers choose RFS when position matters at every size, for example on a press-fit bearing bore. They choose M or L when the function allows the position requirement to relax as size moves. ASME Y14.5 frames MMC and LMC as functional-design tools: a larger actual hole can tolerate more positional variation while the assembly still works.
The design goals behind this are practical:
- Easier fixtures, because functional gages can be built around a single fixed boundary instead of a moving one.
- Higher yield, since parts that sit slightly off position but have favorable size still assemble and still pass.
- Predictable assembly, because the clearance logic is written into the drawing rather than left to judgment on the floor.
- Lower scrap and fixture cost, which Machine Design notes is a common reason practitioners rely on bonus tolerance.
Consider a flange that bolts to a mating plate. Without a modifier, every hole must hold its position within the stated zone even when the holes come out larger than needed. With an MMC modifier, a hole drilled toward its upper size limit leaves more clearance around the bolt, and the drawing lets position drift by that same amount. The bolt still passes through. Nothing about the function changed, but the rejection rate drops.
The rule works in reverse for the inspector. Before you compute anything, read the frame. If the modifier is missing, the answer is zero bonus and the matter is closed. If it is present, you owe the drawing a size measurement, because the allowance now depends on it. We cover reading the frame itself later, and our guide on what a feature control frame tells you goes deeper on the symbols.
Finally, keep the governing standard in view. Older drawings sometimes use obsolete symbols or an earlier revision of the standard, and a few reference international standards instead. The principle is the same across them, but you should confirm which document applies before you trust a calculated result.
How do MMC and LMC generate bonus tolerance?
The logic hinges on a single idea: the modifier names a size condition, and bonus accumulates as the feature moves away from that condition. The direction of movement depends on the feature type and on which modifier is called out.
MMC means the feature holds the most material. For an internal feature such as a hole, MMC is the smallest size. For an external feature such as a pin, MMC is the largest size. Engineeringtechnology describes the same relationship: MMC is the condition where a feature contains the most material, while LMC is the condition where it contains the least.
Here is how that plays out:
- A hole at its smallest permitted size earns no bonus. Every bit of size above that minimum adds directly to the positional allowance.
- A pin at its largest permitted size earns no bonus. As the pin shrinks below that maximum, the allowance grows by the same amount.
- Under LMC the logic flips. A hole at its largest size sits at LMC and earns nothing, and bonus accumulates as the hole shrinks toward its MMC limit.
- A pin at its smallest size sits at LMC, and bonus accumulates as the pin grows toward its MMC limit.
The per-condition rule can be stated in one line each. Under MMC, bonus is the departure from the MMC size toward the LMC size. Under LMC, bonus is the departure from the LMC size toward the MMC size. In both cases the departure is measured as an absolute amount, and a feature sitting exactly at its modifier size contributes zero.
Why would a designer pick LMC at all? Because some functions care about the thinnest section of material, not about clearance. Think of a hole near the edge of a casting, where wall thickness must never fall below a safe minimum. At LMC the hole is largest and the wall is thinnest, so position is held tightest there. As the hole shrinks, the wall gets thicker and the drawing can afford to loosen position. The bonus follows the protection of minimum material instead of the assembly clearance.

RFS stays outside this machinery entirely. With no modifier, the departure from any size condition is irrelevant to position, so the bonus is zero at every actual size. For inspection, that is a reminder worth repeating: a missing modifier is not an oversight to be "fixed" by software, it is a different control.
One more consequence follows from the arithmetic. The largest bonus a feature can earn equals the full size tolerance of that feature, because the feature can only travel from its modifier size to its opposite limit. A hole can earn at most the full size tolerance as bonus. Practitioner stack analysis, such as the direct position approach in this ASEE paper, shows how this extra allowance enters tolerance-stack equations and how MMC, LMC and RFS each change the extreme conditions you must consider in an assembly.
How do you calculate bonus tolerance and total position tolerance?
Two formulas carry the whole calculation. For an internal feature controlled at MMC, the bonus tolerance equals the actual feature size minus the MMC size. The total positional tolerance equals the specified positional tolerance plus that bonus. Machine Design presents the same pair for the hole case, and Wevolver's true position explainer restates them with examples on clearance holes.
For external features at MMC the subtraction reverses, because MMC is the largest size: bonus equals the MMC size minus the actual size. For LMC, swap the roles again and measure the departure from the LMC size. In every case the bonus cannot be negative. If the arithmetic produces a negative number, the feature is outside its size limits, and that is a size rejection before position even enters the picture. Clamp the bonus to zero only in the sense that a feature at its modifier size earns nothing.
Here is the checklist we use at the inspection bench:
- Read the feature control frame and confirm a circled M or L follows the tolerance value.
- Measure the actual feature size, and confirm it sits within the size limits on the drawing.
- Subtract the modifier size from the actual size (or the reverse for an external feature) to find the departure.
- Add the departure to the specified positional tolerance to get the total allowable position.
- Compare the measured positional deviation against that total, and record pass or fail.
A worked example. Say a hole is dimensioned 10.00 to 10.10 mm, with a positional tolerance of 0.20 mm at MMC. These inputs are illustrative. The MMC size is 10.00 mm, the smallest hole. Suppose you measure the hole at 10.07 mm and its center sits 0.24 mm from true position.
Bonus equals 10.07 minus 10.00, which is 0.07 mm. Total positional tolerance equals 0.20 plus 0.07, which is 0.27 mm. The measured deviation of 0.24 mm falls inside 0.27 mm, so the hole passes. Judged against the stated 0.20 mm alone, the same hole would fail. That gap is the entire reason bonus tolerance exists, and also the reason inspection software must apply it correctly.
Note the unit discipline too. Positional tolerance is a diameter of a cylindrical zone, so the measured deviation must be expressed as a diameter as well. A center offset along more than one axis must be converted to a diametral deviation before comparison. Mixing radius and diameter is one of the most common ways a good part gets rejected.
We preview one more idea here. The total allowance grew, but the boundary the part must never cross did not. That fixed boundary is the virtual condition, and the next section explains it.
What are virtual condition and functional gages, and how do they relate to bonus?
Virtual condition is the constant boundary created by a feature's size and its geometric tolerance acting together. It does not move when bonus tolerance grows. That stability is what makes it the real worst-case limit for assembly.
For an internal feature at MMC, the virtual condition equals the MMC size minus the geometric tolerance. For an external feature at MMC, it equals the MMC size plus the geometric tolerance. For a hole, subtract the geometric tolerance from the MMC size to find the virtual condition. A mating pin larger than 9.80 mm will not fit in the worst case, regardless of how much bonus the hole has earned.
The key relationships are worth holding together:
- Internal feature at MMC: virtual condition = MMC size − geometric tolerance.
- External feature at MMC: virtual condition = MMC size + geometric tolerance.
- LMC features follow the same pattern, built from the LMC size instead.
- Virtual condition stays fixed while the allowable position floats with the actual size.
Functional gages exploit this directly. A go gage built to the virtual condition size, and located at true position, checks the worst-case assembly in a single motion. If the gage seats, every combination of size and position within the drawing's limits will assemble. This is why designers who rely on MMC often see fixture and gaging costs fall: the gage embodies the bonus logic physically, so no one has to compute it per part.
On a coordinate measuring machine the physics is replaced by arithmetic, but the meaning is unchanged. When the CMM reports a positional result with bonus applied, it is telling you the part would pass the functional gage. When it reports without bonus, it is applying the tighter stated tolerance and may reject parts a gage would accept. That is the false-reject trap, and it is why you must confirm the software setting matches the drawing.
The practical takeaway is a division of labor. Bonus tolerance answers the question, "How far may this particular feature sit from true position?" Virtual condition answers, "What boundary must nothing violate in assembly?" Both must hold. A part with a generous bonus still fails if its feature intrudes on the virtual condition boundary, and a part with a tight position can still fail if its size has strayed outside limits.
How do you read the feature control frame for bonus tolerance?
A feature control frame reads left to right: the geometric characteristic symbol, the tolerance zone with its diameter symbol and value, a material condition modifier if present, and then the datum references in order of precedence. The circled M or L sits immediately after the tolerance value. That placement tells you the modifier applies to the feature itself.
Datum references can carry their own modifiers too, which is where inspectors often stumble. A modifier after a datum letter applies to the datum feature of size and allows datum shift, a separate allowance from the bonus on the controlled feature. Mixing these two ideas produces wrong calculations, so treat them separately. Our guide on GD&T datums for inspection teams explains how datum shift causes false rejects, and our guide to position tolerance covers the zone itself.
Run this pre-inspection checklist on every drawing:
- Confirm which standard governs, and which revision, before interpreting any symbol.
- Verify the dimensions locating the feature are basic dimensions, shown in boxes, so position is measured from theoretical exact locations.
- Read the tolerance value and the modifier together, and note whether it is M, L or absent.
- Look up the MMC or LMC size from the size dimension, and write it down next to the frame.
- Check the datum references for their own modifiers, and decide whether datum shift applies.
- Check the tertiary datum with extra care, since the order of datums changes how the part is constrained and therefore what position is measured.
A tertiary datum deserves its own warning. When the third datum is a feature of size, its modifier changes how much the part may float in the fixture, and an inspector who ignores it will set up the part wrong. The measured position then differs from what the drawing intends, regardless of how accurate the machine is.
Finally, make recording a habit. Write the governing standard, the modifier and the modifier size in your inspection notes every time. A reader opening the record months later, or an auditor reviewing it, should be able to reconstruct the calculation without the drawing in hand. That single habit prevents more disputes than any software feature.
What does bonus tolerance change in inspection and CMM workflows?
The first step happens before any measurement: confirm the drawing references ASME Y14.5 or whichever alternate standard it names. Software that calculates bonus automatically assumes a standard, and applying one standard's rules to a drawing written under another yields results that look precise and mean nothing. Our reference on ASME Y14.5 is the place to confirm what the standard defines.
Then follow a fixed sequence:
- Import the CMM data and confirm each feature maps to the right balloon and characteristic. Our walkthrough on importing CMM data into inspection reports shows the mapping step.
- Record the actual feature size from the CMM, not the nominal.
- Compute the bonus from the departure between actual size and the modifier size.
- Add the bonus to the specified positional tolerance to get the total allowable position.
- Compare the measured positional deviation against that total and flag the result.
- Store every intermediate value in the report so the decision can be audited.
Several errors recur, and each has a quick check:
- Bonus applied with no modifier on the drawing. Check the frame before trusting any automatic result.
- Bonus applied in the wrong direction, usually from mixing up internal and external features or MMC and LMC. Sanity-check that a hole at its smallest size earns zero under MMC.
- Radial deviation compared against a diametral tolerance. Convert before comparing.
- Size outside limits ignored because position passed. Size is its own characteristic and must pass independently.
- Corrupt or mismatched files producing wrong sizes. Our checklist of four CMM file checks catches these before they reach the report.
Pro Tip: Report the actual size, the calculated bonus, the total allowable position, the governing standard and the measurement method on every positional line. A pass or fail with no supporting numbers cannot be defended in an audit.
A complete inspection record holds the actual feature size, calculated bonus, total position tolerance, governing standard and measurement method for each controlled feature. With those in place, anyone can recompute the result and arrive at the same answer.
Which quick examples build the habit?
Worked cases can help make the calculation automatic. Work through them by hand, and the software output will stop feeling like a black box.
Example A, an MMC hole. Use the MMC size, actual size and specified positional tolerance to calculate the bonus and total allowable position. Compare the measured deviation with that total to determine whether the feature passes.
Example B, an LMC hole. Use the LMC size and actual size to calculate the bonus, then add it to the specified positional tolerance. Compare the measured deviation with the total to determine whether the feature passes.
Recording the result. In an inspection summary, write the actual size, the modifier and its size, the bonus, the total allowable position and the measured deviation, then mark pass or fail. Record each feature separately.
An editorial view on choosing MMC or LMC
In our experience the right modifier follows the function, and arguments about it usually hide a communication gap. Choose MMC when assembly robustness and yield matter most: it rewards parts that drift toward more clearance and pairs naturally with simple go gages. Choose LMC when a minimum section, such as an edge wall, must be protected. Whichever you pick, settle the gage and fixture strategy at the same time as the drawing intent, because a modifier the shop cannot gage is a modifier that will be misapplied. The best drawings come from designers and inspectors talking before release, not after the first rejection.
— Michael Chen
How QA-Report supports bonus tolerance inspection
Hand calculation can become cumbersome for a flange with many holes and a stack of drawings. We help your team apply the method in this article consistently. The QA-Report platform covers the workflow end to end:
- Automatic drawing ballooning, so every controlled feature is numbered and traceable to the drawing.
- Tolerance validation that flags out-of-tolerance deviations as you enter or import results.
- CMM data import, with our CMM inspection software mapping measured values to ballooned characteristics.
- Audit-ready PDF reports that carry the actual values behind every pass or fail.
In practice that means fewer manual calculations, cleaner records for ISO 9001, AS9100 and PPAP reviews, and safer accept or reject decisions. You can start on the Free plan, or compare Basic at $49.99 per month and PRO at $149.99 per month on the pricing page.
FAQ
What does "least material condition" mean?
Least material condition, or LMC, is the size at which a feature contains the least material. For a hole it is the largest permitted size, and for a pin it is the smallest. EngineeringTechnology.org defines it this way alongside MMC.
Is .005 a tight tolerance?
It depends on the feature, the process and the function. Whether a value is tight is judged against what the manufacturing process can hold and what the assembly needs, not against the number alone. Check the drawing's stated tolerance, then compare it with your process capability before deciding.
What are GD&T fits?
GD&T fits describe how mating features relate, such as clearance, transition or interference between a hole and a pin. Material condition modifiers tie the geometric control to that fit, so the allowed position follows the actual sizes. ASME Y14.5 is the governing reference for these modifiers.
What is the 3/2/1 rule for GD&T?
The 3/2/1 rule describes how a part is constrained by its datum system: the primary datum contacts at three points, the secondary at two and the tertiary at one. It sets how the part sits in the fixture, which determines what position is measured. Our guide to GD&T datums explains how this affects inspection.
Does bonus tolerance apply when no modifier is shown?
No. With no M or L modifier, the control is Regardless of Feature Size and the bonus is zero at every actual size. The positional tolerance stays at its stated value.
Sources
- Engineeringtechnology
- Ensuring Parts Fit, Using Bonus Tolerance to Your Advantage | Machine Design
- Calculation Of Tolerance Stacks Using Direct Position Approach In Geometric Dimensioning And Tolerancing
- True Position in GD&T: Formula, Tolerance Zones, and MMC