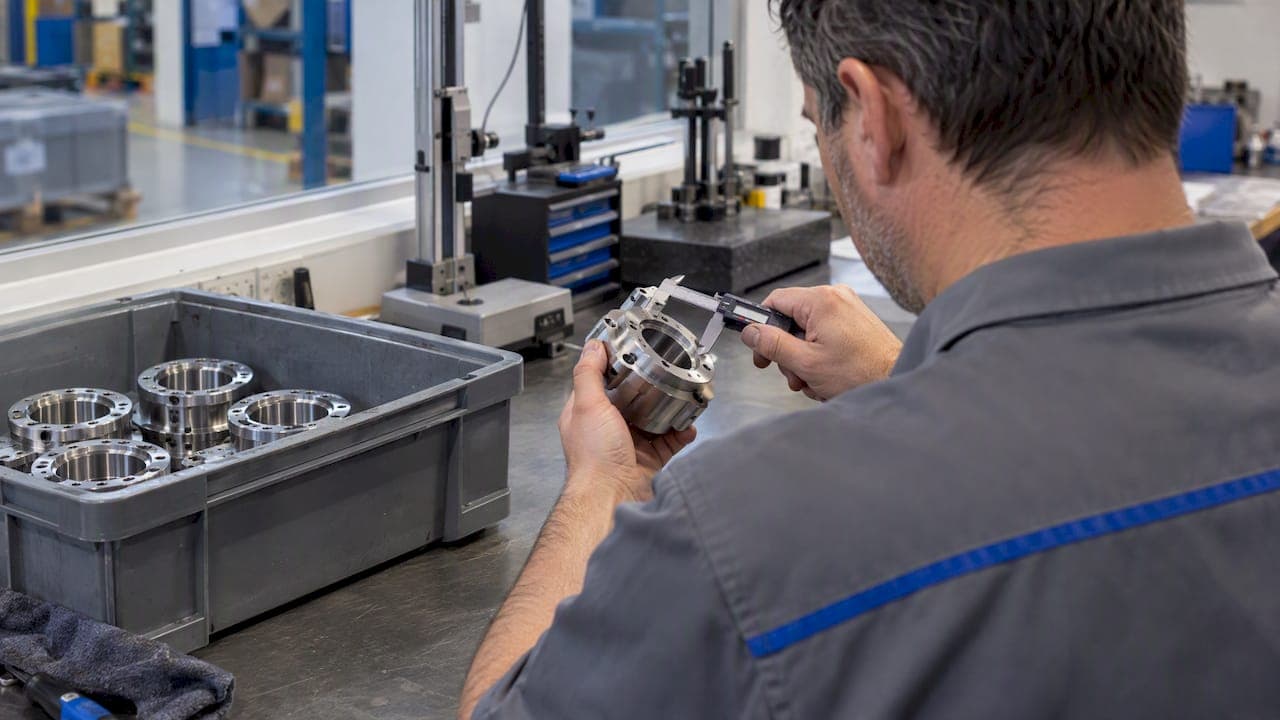
A final inspection checklist is the last gate before work is accepted: a building goes to the code official for sign-off, or a manufactured lot goes to the customer. The two meanings share one logic. You confirm the requirement, verify the work against it, record objective evidence, and only then release. This guide covers both, with the most depth on manufactured parts, because that is where a weak checklist is most expensive.
TL;DR
- A final inspection verifies finished work against the current requirement. It is a readiness gate, not a progress check.
- For manufactured product, check in this order: requirements and revision, identity and traceability, visual, dimensional, functional, labels and packaging, then disposition and release.
- Record a measured value, the tool used and the acceptance limit for each characteristic. A bare tick leaves no evidence.
- Inspection findings and release authority are separate control points. The inspector reports; an authorized person releases, holds, reworks or accepts under concession.
- For US building finals, the local building department sets the requirements, so use its own checklist and confirm access and scheduling with it.
Table of Contents
- What a final inspection actually covers
- The manufacturing final inspection checklist
- The sequence that keeps a final inspection defensible
- Evidence: what to record on every line
- Inspection is not release
- Our perspective: where final inspection checklists break
- Building final inspections in the US
- Paper, spreadsheet or software
- Building the checklist in QA-Report
- Common mistakes to avoid
- FAQ
- Sources
What a final inspection actually covers
The phrase means different things depending on who is asking, and the top search results are mostly about buildings. Both uses are covered here.
Building final. A local building department or zoning authority checks that the finished structure complies with codes, usage rules and safety requirements. Procore's guidance describes it as usually the last requirement before occupancy.
Manufacturing final. The producer, and often the customer, verifies that the finished part, lot or serial number meets the drawing, specification and purchase order before it ships. Depending on the company, this is called final quality control, outgoing inspection or pre-shipment inspection. Same job, different label.
In both cases the final inspection is not the place to discover that earlier steps were skipped. Official building checklists make this explicit, as the next sections show.

The manufacturing final inspection checklist
Use the list below as a template and cut it down to the characteristics that matter for your part. ISO 9001 does not prescribe one universal final-inspection form or product-specific acceptance limit. ISO's overview of the standard describes a risk-based approach to monitoring and measurement, so your own drawings, specifications, standards and customer requirements define what "pass" means. It also means critical characteristics deserve more attention than cosmetic ones. Do not weight every line equally.
1. Requirements and readiness
- Current drawing revision and specification are in hand, and they match the purchase order.
- Customer-specific requirements are identified (special characteristics, packaging, certificates of conformance).
- The inspection plan states which characteristics are checked, how, with what tool and at what sample size.
- Previous operations are signed off. Final inspection should not be the first time anyone checks a feature.
2. Identity and traceability
- Part number, revision, lot, batch or serial number match the paperwork.
- Quantity presented equals quantity on the route card or order.
- Material certifications and process certificates are attached where required.
- Every record can be tied to one specific product instance.
3. Visual and workmanship
- Surface finish, burrs, scratches, dents, corrosion, discoloration and contamination are checked against a defined standard.
- Required features are present: threads, holes, markings, coatings, hardware.
- Cosmetic acceptance criteria are written down, ideally with a reference sample or photo.
4. Dimensional and GD&T
- Every ballooned characteristic on the drawing is measured, or the sampling plan says why it is not.
- Each result is compared with its tolerance, including geometric tolerances such as position, flatness and profile.
- Out-of-tolerance values are flagged at the moment of entry, not found later in a spreadsheet.
- Near-limit results get a second look at method and measurement uncertainty (see the section on evidence below).
5. Functional and safety tests
- Pressure, leak, torque, electrical, fit or function tests are completed per the specification.
- Test results are recorded with the equipment used and the operator.
6. Measurement validity
- Gauges, CMMs and other instruments are within calibration on the date of inspection.
- The instrument is suitable for the tolerance being checked.
- The environment and method are appropriate for the feature.
7. Labels, markings and packaging
- Labels carry the correct part number, revision, lot or serial, and any required barcode or compliance marking.
- Packaging protects the part and meets the customer's instructions.
- Shipping labels match the packing list. If you print your own carrier labels, a short reference on 4x6 shipping label setup can help with size and printing basics, though carrier requirements differ by country.
8. Nonconformance, disposition and release
- Nonconforming product is identified, segregated and recorded.
- Disposition (rework, scrap, return to supplier, use-as-is by concession) is decided by someone with authority.
- Reinspection is documented after rework.
- A named, authorized person signs the release before shipment.
Our article on ISO 9001 clause 8.7 and control of nonconforming outputs goes deeper on steps 8 and the segregation logic.
The sequence that keeps a final inspection defensible
Order matters. Numbering the answers before reading the questions produces a tidy page and a useless record. A reliable sequence looks like this:
- Confirm the applicable requirements and the current revision.
- Verify identity, quantity and readiness of the lot.
- Inspect visual, dimensional, functional, safety, labeling and packaging characteristics.
- Record objective evidence and every defect found.
- Segregate or control nonconforming output.
- Complete corrective action and reinspection where needed.
- Obtain authorized release, or a documented hold.
Sampling follows the approved inspection plan or the customer requirement. An arbitrary sample size chosen by whoever is on shift is not a plan. If the customer specifies an AQL or a 100% check on a critical feature, the checklist should say so on its face.
Evidence: what to record on every line
A checklist that only collects ticks is a weak record. Compare these two entries for a bore diameter:
| Weak entry | Defensible entry |
|---|---|
| Bore diameter: OK | Bore diameter, drawing rev C, balloon 14: measured value, acceptance limits, instrument ID and calibration date, operator, date and time, serial number |
NIST's survey of the Quality Information Framework describes traceability information as including the date and time, product instance, machinery, measurements, operator and environment. The same NIST report frames inspection as an information flow from product definition through planning, execution, analysis and reporting. If you import CMM data without keeping that context, the audit trail weakens. Broken traceability behaves like a broken chain: it fails at the weakest link, and you find out during an audit.
Recording a number also does not make it conclusive. NIST's work on dimensional measurement traceability stresses that calibration, reference standards, environment and method must support the conformity decision. For dimensions that land close to a limit, document the method and review measurement uncertainty before ticking pass.
For more on record structure, see our guide to inspection documentation best practices.
Inspection is not release
One of the most common gaps in small and mid-size shops is treating a completed inspection as permission to ship. They are two control points.
The ISO 9001 Auditing Practices Group notes that acceptance under concession must be authorized by a relevant authority and, where applicable, the customer. In practice, build your checklist with two clearly separated blocks:
- Inspector findings: what was measured, what passed, what failed.
- Disposition and release: who decided to release, hold, rework or accept by concession, and when.
The person who found the defect should not be the only person deciding what happens to the part, unless your procedure explicitly gives them that authority.
Our perspective: where final inspection checklists break
We see the same pattern in shops moving from paper and spreadsheets: the checklist exists, but it is disconnected from the drawing. Someone balloons a PDF by hand, someone else types results into a separate sheet, and a third person assembles a report at the end of the day. Each handoff is a chance to transpose a value or lose a revision.

Our view is that the final checklist should be generated from the drawing, not written beside it. When ballooned dimensions link directly to measured results, out-of-tolerance values are flagged as they are entered, and the statistical summary and PDF report come from the same data, the checklist becomes a by-product of good inspection rather than extra paperwork.
We also think release authority is under-designed in most shops. Role-based access, so that inspectors record and authorized staff release, is not bureaucracy. It is how you show an auditor that the two decisions were separate.
— Michael Chen
Building final inspections in the US
If you landed here for a home or commercial construction final, the rules are set locally. There is no single US-wide checklist, duration or cost. Building departments set their own requirements, scheduling windows and reinspection fees, so start with your jurisdiction's own form.
What the official checklists have in common
The Placer County final inspection checklist and the Napa County minimum requirements list are two public examples. Typical items include:
- Smoke detectors on required levels and GFCI/AFCI protection where required
- Labeled electrical panels
- Operable heating and cooling, with final gas tests where applicable
- Completed exterior doors, landings and lights
- Grading that drains away from the building
- Accessible, unobstructed exits
- Correction of items from earlier inspections
Exact requirements vary by jurisdiction and project, so treat this as orientation rather than a substitute for your department's list.
Readiness comes before workmanship
The Placer County form treats the final as a readiness gate: it cannot be phased, and incomplete work can delay the inspection and trigger a fee. Before you book, confirm that:
- Earlier required inspections and correction notices are closed.
- Approved plans and permits are on site.
- Required clearances from other departments are obtained, where they apply to your project.
- Power and utilities are on so systems can be tested.
- Debris is removed and safe access, such as a ladder for roof or attic inspection, is provided where required.
Procore's preparation guidance lists the usual reasons a final fails: finished work that does not match approved plans, obstructed exits, untestable systems, missing signage or accessibility features, incomplete drainage and unresolved earlier corrections. Start with the paper and prerequisites, not only a cosmetic walkthrough.
How long does it take?
No authoritative US source sets a standard duration. It depends on scope, building size, number of systems and whether defects or inaccessible areas require follow-up. Ask the issuing authority about the appointment window and access requirements when you schedule.
Paper, spreadsheet or software
For a handful of simple parts, a controlled paper form works. It stops working when drawings change often, parts have dozens of characteristics, or customers want AS9102, PPAP or similar packages.
| Need | Paper or spreadsheet | Purpose-built inspection software |
|---|---|---|
| Link drawing balloons to results | Manual re-keying | Direct link from ballooned dimension to measured value |
| Catch out-of-tolerance values | Reviewer finds them later | Flagged when entered |
| Import CMM output | Copy and paste | Import and mapping to characteristics |
| Revision control | Depends on discipline | Report tied to the drawing version |
| Share with a customer | Email attachments | Report generated as PDF or shared interactively |
| Release authority | Signature line, if present | Role-based permissions |
If your team also runs receiving checks, the same logic applies upstream. See our notes on incoming inspection best practices. For broader context, our guides to manufacturing QA and quality control in manufacturing cover where the final inspection sits in the whole system.
Building the checklist in QA-Report
QA-Report is a cloud-based inspection and reporting platform for manufacturers, machine shops and quality engineers in aerospace, automotive and medical device production. You balloon the drawing, link each dimension to measured results, import CMM data, and the platform flags out-of-tolerance deviations and produces statistical summaries and PDF reports for FAI, dimensional and GD&T inspection.
Plans on the pricing page start with Free at $0 per month, then Basic at $49.99 per month and PRO at $149.99 per month. On-Premise and Enterprise Solutions are available without a published price. You can try the platform before deciding.
Common mistakes to avoid
- Checking against an old drawing revision because the printout was on the bench.
- Sampling by habit instead of by the plan or the customer requirement.
- Using an instrument that is out of calibration or too coarse for the tolerance.
- Letting the inspector also approve release without a documented authority.
- Storing results without the serial number, date or equipment, so the record cannot be reconstructed.
- Skipping a hold tag on nonconforming parts, so they drift back into the shipping area.
FAQ
What does a final inspection consist of?
In manufacturing, it verifies that finished product meets the current drawing, specification and customer requirements across identity, visual, dimensional, functional, labeling and packaging checks, then ends in authorized release. In building, it is a code official's walkthrough of the completed work against approved plans and applicable code. The checklist differs, but the principle of recorded evidence against defined criteria is the same.
What needs to be finished before a final building inspection?
The work must be fully complete. Earlier inspections and correction notices must be closed, plans and permits on site, required clearances obtained, systems available for testing and safe access provided. Check your own building department's list, since requirements and reinspection fees vary.
Is an outgoing inspection checklist different from a final inspection checklist?
In most manufacturing contexts they describe the same step: the last verification before product leaves your facility. Some companies use outgoing inspection for the shipment-focused check of quantity, labels and packaging, and final inspection for the full verification of characteristics. Define the term in your own procedure.
Does ISO 9001 require a specific final inspection form?
No. ISO 9001 does not prescribe one form or acceptance limits. You define requirements from your specifications, drawings, standards and customer needs, and keep evidence that the product conforms.
Sources
- Final Inspection Checklist, Placer County
- Minimum Requirements for Final Inspection, Napa County
- Final Building Inspection: Preparation and Checklist, Procore
- ISO 9001 overview, ISO
- ISO 9001 Auditing Practices Group
- End-to-End Quality Information Framework Technology Survey, NIST
- Dimensional measurement traceability by X-ray computed tomography, NIST