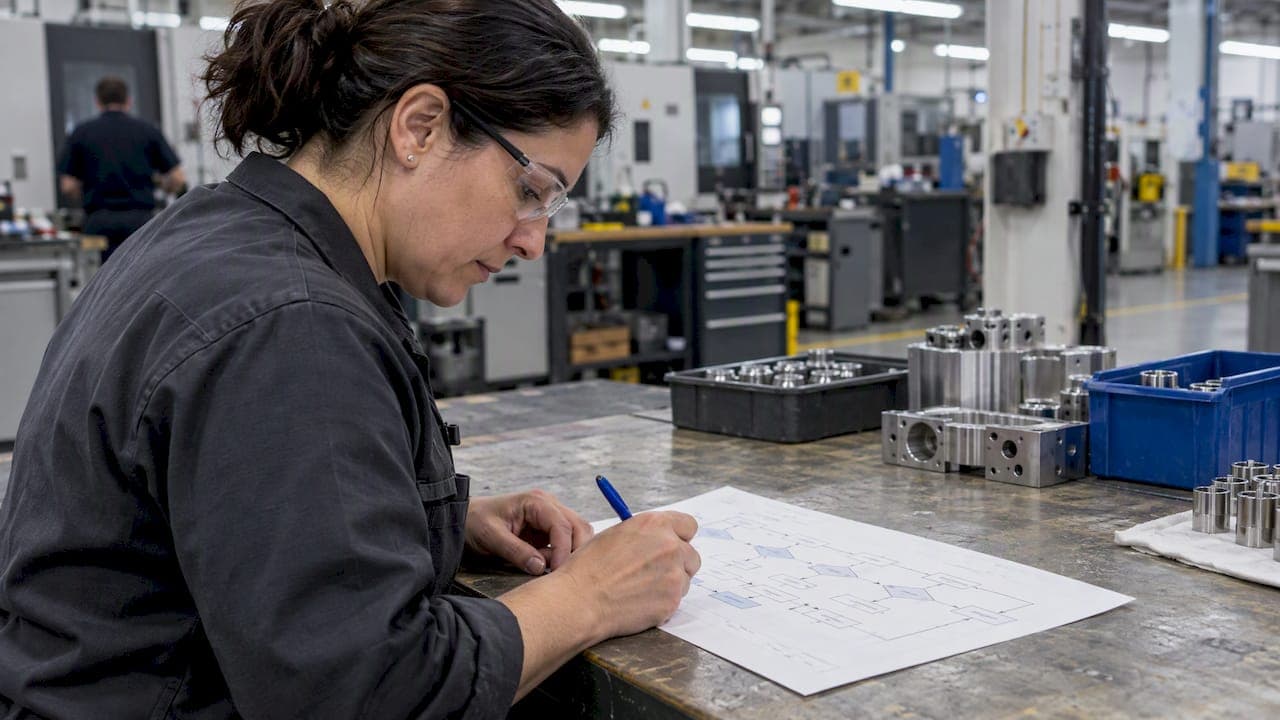
A PPAP process flow diagram is a sequential map of every material, process, and inspection step from receiving to shipping. It is one of the 18 PPAP elements, and its core job is to let a reviewer cross-check each step number and control against the PFMEA and the Control Plan. Build it once, number it cleanly, and the rest of the package stays traceable.
TL;DR:
- Customer manuals set the required detail and may require a PSO or run at rate before the warrant; AIAG sample layouts are illustrative.
- Show every operation, inspection, storage, transport, outsourced step, and nonconforming part route, including measurement methods and inspection frequency at relevant steps.
- Use sequential operation numbers and names across the flow diagram, PFMEA, and Control Plan, and match part and revision details to the drawing and PSW.
- Walk the process from receiving through shipping with operators and inspectors, then compare the diagram with a trial run and correct any missing steps.
- Record the diagram’s revision, date, and approval trail, then lock the approved PDF to prevent untracked changes from creating mismatches across the submission.
Table of Contents
- What a PPAP process flow diagram shows and when you need it
- Checklist: what to include on a PPAP process flow diagram
- How to create a PPAP process flow diagram on the shop floor
- Annotated example: what an acceptable PFD looks like
- Aligning the PFD with the PFMEA and Control Plan
- Common PFD pitfalls and one quick fix
- How QA-Report keeps your PFD, inspection data, and PPAP package connected
- FAQ
- Sources
What a PPAP process flow diagram shows and when you need it
The diagram lays out each operation, inspection, storage, movement, and outsourced step in the order the part actually experiences them. Think of it as the spine of your submission: if the spine is crooked, every document attached to it looks suspect.
PPAP itself exists so that suppliers can show they produce parts that meet engineering design records consistently during a real production run at production rates. The flow diagram is where that claim becomes visible, step by step.
Here is what you should know before you draw anything:
- The PFD is one of the 18 PPAP elements and is commonly required at submission.
- It must cover operations, inspections, storage, handling, and any work done by outside suppliers.
- Submission level and customer requirements change how detailed it must be. Our PPAP levels guide explains which levels call for which documents.
- Customer-specific rules can add steps. An AIAG errata sheet notes that sample flowcharts are examples rather than mandatory formats, and that some customers want a PSO or a run at rate before the warrant is submitted.
- If you need a primer on the other elements, start with our PPAP overview for quality engineers.
Always read your customer's supplier manual before you finalize the layout. The AIAG sample is a starting point, not a template you must copy.
Checklist: what to include on a PPAP process flow diagram
Use this list to audit an existing diagram or to build a new one. If a reviewer can find every item below quickly, you are in good shape.
- Every operation from receiving to shipping, with consistent names and sequential numbers.
- Incoming inspection and raw material handling, followed by machining or processing, in-process inspection, assembly, packaging, and shipping.
- Outsourced operations, flagged clearly with the supplier name and the return path to your plant, including any inspection on return.
- Rework, segregation, containment, and scrap paths, each drawn with its decision point so nobody has to guess where a nonconforming part goes.
- Transport and storage steps, plus any offline measurement or inspection activity.
- Special characteristics, marked at the operation that creates or controls them, including pass-through characteristics that arrive from a sub-tier supplier.
- Part number and drawing revision that match the rest of the PPAP submission exactly.
- Document control: a revision level, a date, and an approval trail, because an uncontrolled PFD invites questions about every other document.
The practical standard here is the level of detail shown in a NASA-hosted PPAP tutorial. It lists the process flow diagram alongside the PFMEA and Control Plan as required entries and illustrates expected detail with a resistor example: the diagram should show whether parts are singulated before terminations are applied, and how often resistance is checked. That is the depth reviewers look for: not just "inspect," but where and how often.
Pro Tip: Print the diagram and tick each checklist item with a pen. Gaps that hide on screen stand out on paper.

How to create a PPAP process flow diagram on the shop floor
A diagram drawn from a desk reflects how the process is supposed to run. A diagram drawn from the floor reflects how it runs. Reviewers and auditors can tell the difference, so follow these steps in order.
- Walk the real process. Go from receiving to shipping with operators, production planners, and inspectors. Watch how material actually moves, including the detours nobody wrote down.
- Draw each operation and decision path. Use one name per operation and number the steps sequentially. If two people call the same station by different names, settle on one before you draw.
- Mark inspection and measurement points. For each, note the measurement method and frequency, and link it to the matching Control Plan line. Our article on Control Plan versus Inspection Plan clarifies how those two documents divide the work.
- Identify outsourced operations by name. Show where parts leave your plant, who performs the work, and how parts are verified when they return.
- Add rework, segregation, and scrap paths. Include offline or special handling steps such as dedicated quarantine areas or sorting stations.
- Align numbers and names with the PFMEA and Control Plan. Aim for consistent mapping. Revise under document control and record the revision and date every time something changes.
- Validate against production evidence. Compare the diagram with sample production data or a trial run before submission. If the run reveals a step the diagram omits, fix the diagram, not the story.
One note on pace: you can draw the first version quickly, but the walk-through is what takes time. Do not skip it. A diagram that matches reality saves you from a rejected submission and a second round of customer questions.
Annotated example: what an acceptable PFD looks like
Picture a simple machined-and-assembled part. The flow reads left to right or top to bottom: receiving, prep, machining, in-process inspection, assembly, final inspection, packaging, shipping. A rework loop leaves the in-process inspection and returns to machining, and a separate branch sends rejected parts to segregation and scrap. If heat treatment or plating happens at an outside supplier, a flagged block sits between machining and assembly, with an arrow out to the supplier and an arrow back through incoming inspection.
Each block should carry these labels and annotations:
- Operation number, for example OP 10, OP 20, OP 30, in strict sequence.
- Operation name, matching the PFMEA and Control Plan wording exactly.
- Inspection step marker, a distinct symbol so inspections stand apart from value-adding work.
- Special characteristic symbol, placed on the operation that produces or controls the characteristic.
- Outsourced flag, with the supplier name inside or beside the block.
- Document revision, date, part number, and drawing revision in the title block.
For file format, a PDF or a controlled drawing works well, and the AIAG notes that sample flowcharts are illustrative, so a clean layout of your own is perfectly acceptable. Store the final file in the PPAP submission folder under revision control, next to the PFMEA, Control Plan, and PSW. Our PSW check is a handy last pass: it helps you confirm that part numbers and revision levels agree across every document before anything leaves your hands.
Resist the urge to decorate. A plain diagram with correct labels beats a colorful one with a missing rework path.
Aligning the PFD with the PFMEA and Control Plan
Consistent step numbering is what makes a package traceable. When OP 30 on the flow diagram is also OP 30 in the PFMEA and OP 30 in the Control Plan, a reviewer can follow a single operation across all three documents without translating anything. Break the numbering, and traceability breaks like a chain with a missing link.
Here is how the diagram feeds the other two documents:
- PFMEA: each operation defines the scope of an entry. A turning operation might carry failure modes such as oversize diameter or tool wear.
- Control Plan: the same operation carries the control method, measurement frequency, and reaction plan, such as a regular gauge check.
Reviewers commonly look for these items first:
- Outsourced operations named, not merely implied.
- Special characteristics highlighted and carried into the other two documents.
- A PFD revision that matches the drawing revision and the PSW.
Common PFD pitfalls and one quick fix
In my experience, common mistakes that can lead to rejections include outsourced steps left unlabeled, step numbers that drift between documents, and rework paths that exist on the floor but not on paper. Each one is easy to prevent and awkward to explain once a reviewer finds it.
Before you submit, pick some step numbers at random and verify them against the PFMEA and the Control Plan. If one fails, check them all. Then lock the version and export it to PDF so nobody edits it by accident.
— Michael Chen
How QA-Report keeps your PFD, inspection data, and PPAP package connected
Cross-referencing is where hours disappear, and that is the work we built QA-Report to remove. Our platform connects the drawing, the inspection results, and the final report in one place.
- Automatic drawing ballooning numbers every dimension, so inspection results trace back to the drawing.
- Our platform keeps documents together.
- The measurement wizard links ballooned dimensions to measured results and flags out-of-tolerance values, and CMM data import brings machine results in without retyping.
- Reports export as professional PDFs, ready to sit in your PPAP folder.
The practical benefit is less manual cross-checking and a faster path to a submission-ready package. If you are comparing tools, see our review of APQP and PPAP software. When you are ready to try it, start with our plans and pricing and open a free account today.
FAQ
What are the steps in the PPAP process?
PPAP is built around 18 required elements, including the design record, PFMEA, Control Plan, and process flow diagram. Teams plan the process, gather the documents and measurement data, run production, and submit the package with a warrant. Your customer's manual decides which elements apply.
What are the 18 elements of PPAP?
They are the evidence items defined in the AIAG PPAP manual, covering design records, process documents such as the flow diagram, PFMEA, and Control Plan, measurement and test results, and the part submission warrant. The exact set you submit depends on your customer and submission level.
What are the PPAP submission levels?
Levels define how much documentation you send and how much you retain, and customers choose the level. Higher levels require more of the package to be submitted. Our PPAP levels guide walks through each one.
Does the PFD have to follow a specific format?
No. AIAG's errata notes describe sample flowcharts as illustrative, not mandatory. Follow your customer's requirements and keep the layout clear, numbered, and consistent with the PFMEA and Control Plan.